
High-Purity Water for Dairy Processing and Boiler Feed
A Waikato dairy manufacturer required a reliable source of demineralised water to support cheese production and steam boiler operations. Dissolved minerals present in the available water supply created a risk of scale formation, increased maintenance requirements and reduced boiler efficiency.
FILTEC delivered a fully automated demineralised water plant using ion exchange demineralisation technology to remove dissolved minerals and produce high-purity water. The system provides consistent treated water quality for steam boiler feed while supporting efficient plant operation and long-term equipment protection.
Meeting Strict Boiler Feedwater Quality Requirements
Steam boiler systems require high-purity water to minimise scale formation and maintain thermal efficiency. Dissolved minerals can accumulate on boiler surfaces and pipework, reducing performance and increasing maintenance requirements. The project therefore required:
Consistent high-purity water production
Minimal treated water conductivity
Protection of boilers and pipework
Automated operation and regeneration
Reliable performance at industrial scale
The solution needed to support continuous dairy production while maintaining stringent steam boiler feedwater quality standards.
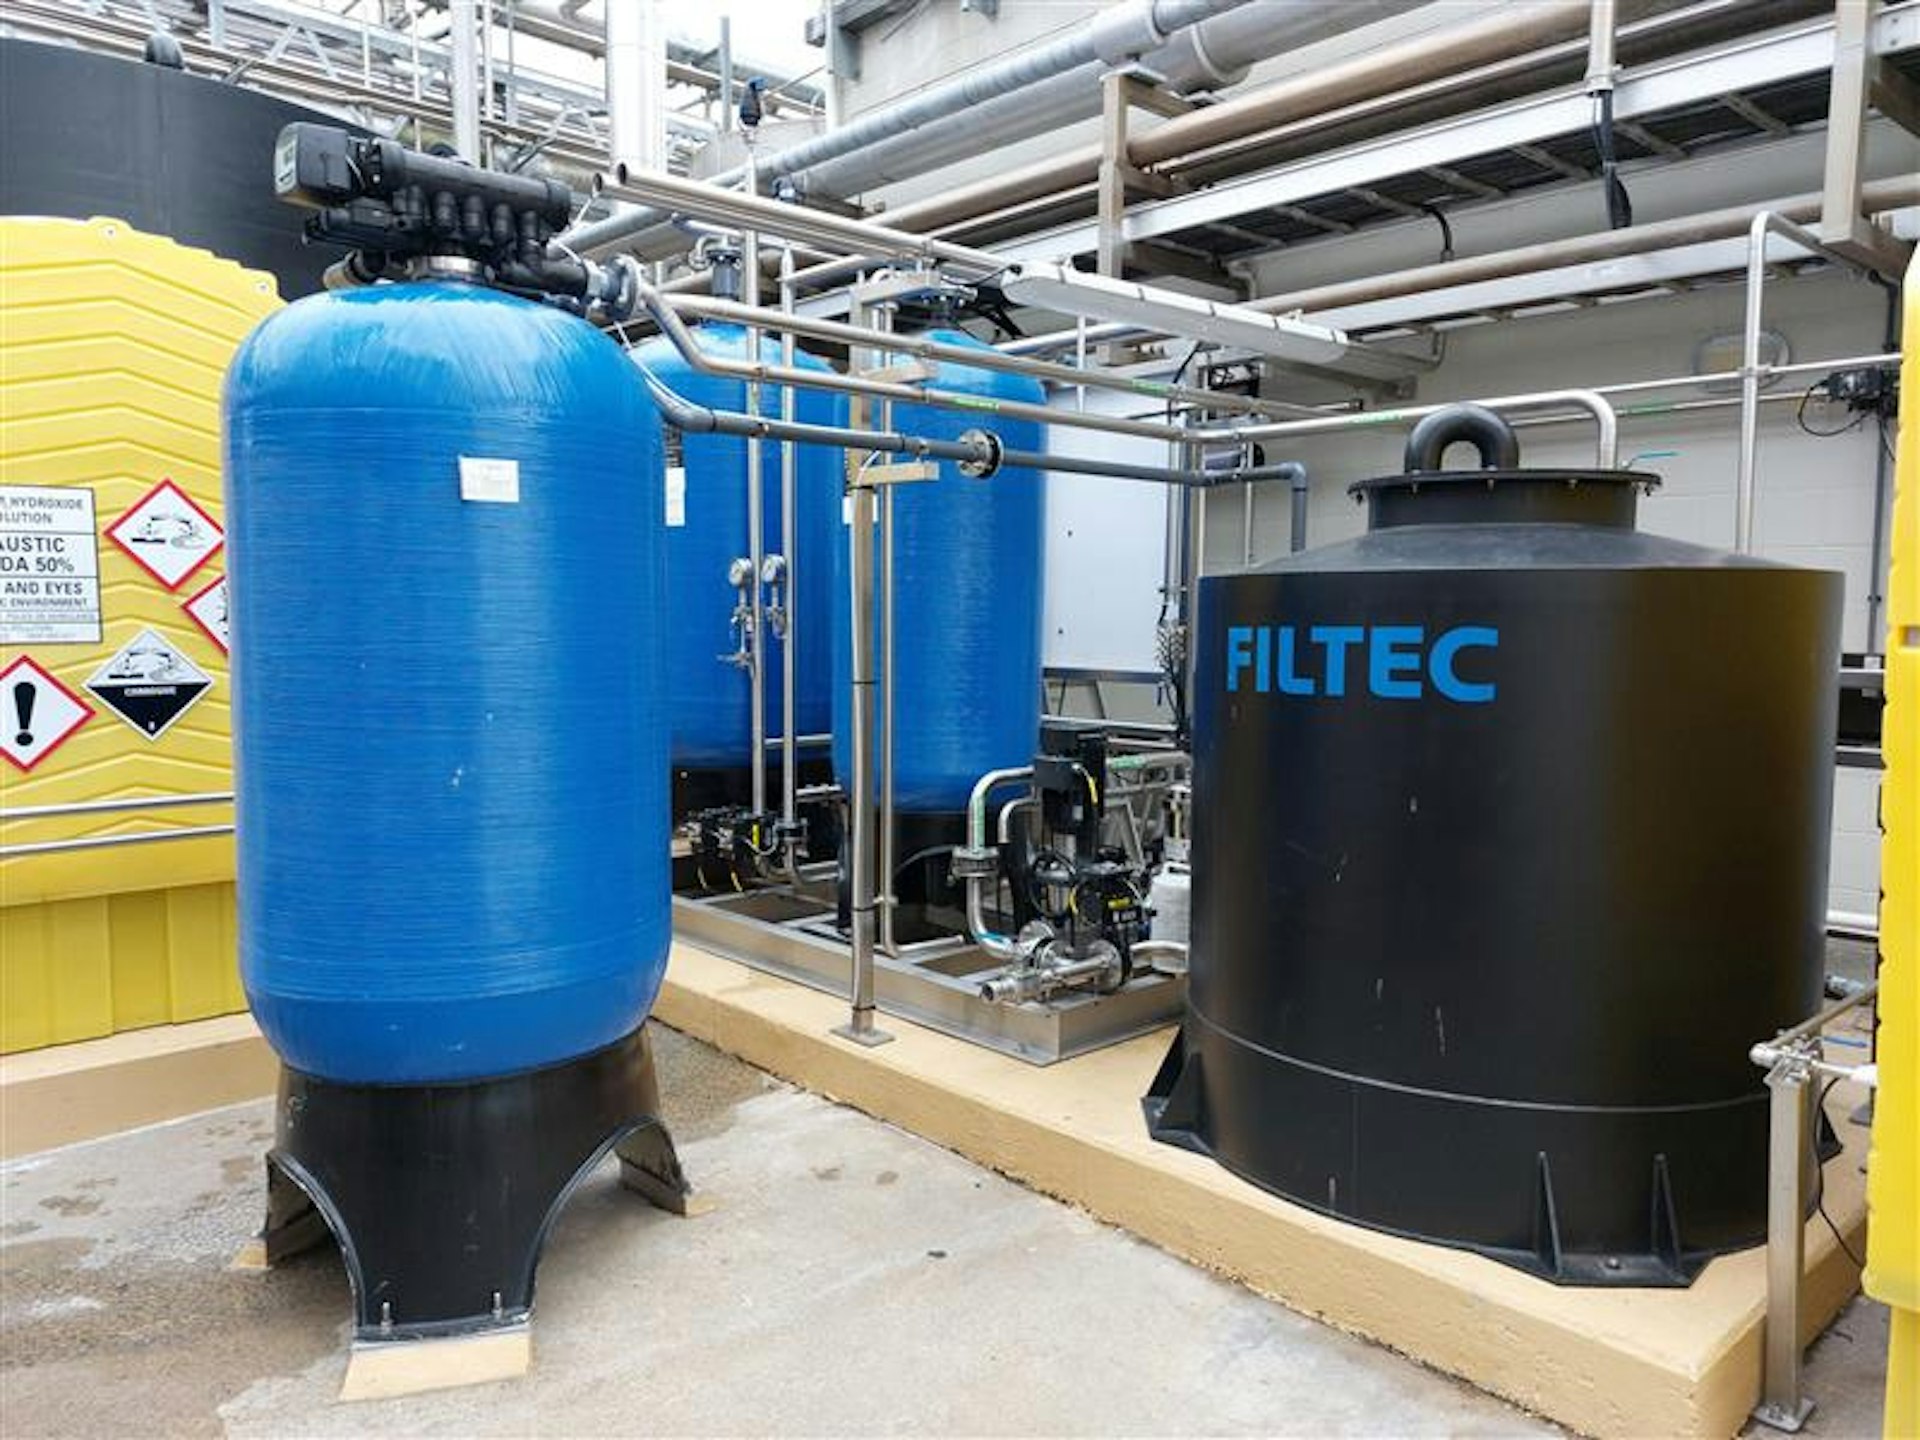
Automated Ion Exchange Demineralisation Plant
FILTEC designed the treatment plant around an automated ion exchange demineralisation process, selected to remove dissolved minerals and charged particles from the water supply. The treatment process includes:
Carbon filtration pre-treatment
Ion exchange demineralisation vessels
Acid regeneration system
Sodium hydroxide regeneration system
Automated process control
The system consistently produces high-purity water for steam boiler feed while maintaining reliable operation through automatic regeneration.


Integrated Design, Fabrication and Installation
FILTEC designed, fabricated and assembled the demineralised water plant in-house before installation at the dairy processing facility. This approach enhanced quality control while ensuring the plant met operational requirements.
In-house process and mechanical design
Workshop fabrication and assembly
Chemical dosing and regeneration systems
SCADA integration and communications
Site installation and commissioning
Integrated delivery reduced project complexity and provided a single point of responsibility throughout the project.
Automation, Monitoring and Operational Reliability
The plant was designed to minimise operator intervention while providing visibility of treatment performance and equipment status.
Automated regeneration sequencing
Conductivity monitoring and control
SCADA integration and remote access
Process performance monitoring
Operational safety enhancements
Welded flanged and triclover chemical pipework connections were incorporated to reduce leakage risk and improve durability within the chemical handling system.

Reliable High-Purity Water for Efficient Boiler Operation
The demineralised water plant now delivers:
300 m³/day treatment capacity
Typical conductivity of 1 µS/cm
Reduced boiler scaling potential
Improved operational efficiency
Lower maintenance requirements
By delivering a fully automated demineralised water plant, FILTEC enabled reliable production of high-purity water for dairy processing and steam boiler feed. The project supports efficient boiler operation, reduced equipment wear and consistent manufacturing performance.
